Technical Data
CompareConcentration
| Measuring Principle | Absorption |
| Application | Color measurement CIE Lab |
| Measuring range | L: 0 to 100 a: -150 to 100 b: -100 to 150 |
| Material | Measuring head: 1.4404/AISI316L Window: Sapphire O-rings: FFKM Gasket seal: PEEK |
| Process temperature | -20 to 60 °C (-4 to 140 °F) 60 to 140 °C (140 to 284 °F) with water cooling |
| Process pressure | 0.5 to 10 bar (7.3 to 145 psi) (absolute) |
| Ex certification | ATEX/IECEx II 1/2G Ex ia op is/db [ia Ga] IIC T6…T3 Ga/Gb |
| Ingress protection | IP 69 (NEMA 6P) |
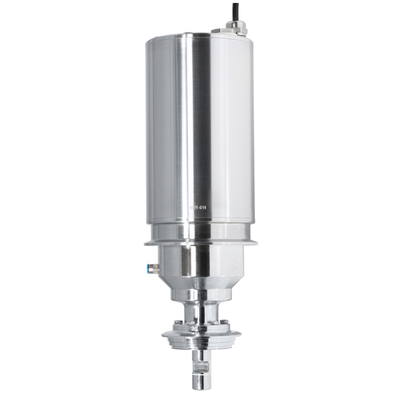
Memosens Wave CKI50 process spectrometer
Memosens Wave spectrometer for color measurement in the food and beverage, chemical and life sciences industries
Advantages
Compact design: the color of the entire spectrum can be determined with just one device.
Easy commissioning: with Memosens technology and Liquiline transmitters, installation is fast and simple. No calibration required, only the reference spectrum of the zero point needs to be recorded.
Powerful color measurement: highly repeatable and long-term reliable color measurement even in demanding process environments, thanks to its high resistance to water ingress, vibration and high temperatures.
Safe and efficient process control: the hygienic design ensures safe product production. By checking the color directly in the process, product losses and potential health risks to consumers can be prevented
Field of application
The Memosens Wave CKI50 is compactly designed and the spectrometer provides reliable, fast color control directly in the process. At the same time, the process spectrometer ensures that hygiene and material standards comply with the specifications of the food industry. Thanks to preset color models and connection to Liquiline transmitters, commissioning is very simple and measurement is stable.
Quality control: color deviations in the final product are caused by color changes in the raw materials. It is therefore crucial to identify them and initiate appropriate adjustments
Filling control: the increasing product diversity and higher production speeds bring the risk of incorrect bottling. Reliable and fast color detection is crucial.
Phase control: via color detection, the phase state in pipes can be quickly identified and product losses minimized, for example during product changeover or cleaning processes.
E+H product configurator
Please enter the product order code to configure
Product comparison
Please enter the order codes of the products you wish to compare in the fields below (up to three products)
Technical documentation
Technical data
Documents/Manuals/Software
Accessories/Spare parts
Source:Endress+Hauserpublic information from the website
Case Studies
Municipal Wastewater Treatment — Wastewater Treatment Plant · Turbidity Application Case
Project Background
Municipal Wastewater Treatment customers at the Wastewater Treatment Plant stage have long faced the challenge of insufficient accuracy in effluent quality monitoring and instruments prone to contamination causing data drift, affecting compliance discharge, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Municipal Wastewater Treatment conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Food & Beverage — Food Production Line · Turbidity Application Case
Project Background
Food & Beverage customers at the Food Production Line stage have long faced the challenge of high hygienic measurement requirements, with inline instruments needing to withstand CIP/SIP cleaning while maintaining stable accuracy, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Food & Beverage conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Chemical & Pharmaceutical — Reactors and Storage Tanks · Turbidity Application Case
Project Background
Chemical & Pharmaceutical customers at the Reactors and Storage Tanks stage have long faced the challenge of highly corrosive media and complex conditions, requiring corrosion-resistant and explosion-proof instruments, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Chemical & Pharmaceutical conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Power & Energy — Power Plant Boiler and Turbine · Turbidity Application Case
Project Background
Power & Energy customers at the Power Plant Boiler and Turbine stage have long faced the challenge of unstable measurement under high temperature and pressure, with high maintenance and downtime costs, placing higher demands on the stability and measurement accuracy of Turbidity.
Solution
Based on the on-site conditions, the Ainstru technical team selected suitable Turbidity for the customer and delivered one-stop service covering selection, installation, commissioning and tuning.
Results
- Measurement accuracy and response speed significantly improved, with stable and reliable data;
- Instruments adapt to complex Power & Energy conditions, greatly reducing maintenance;
- Helping customers achieve continuous online monitoring and cost reduction, highly recognized by customers.
Related Products
 Endress+Hauser
Turbimax CUS52D
 Endress+Hauser
Turbimax CUS51D
 Endress+Hauser
Turbimax CUS71D
 Endress+Hauser
Turbimax CUS50D
 Endress+Hauser
Turbimax CUE22, compact white light
 Endress+Hauser
Turbimax CUE21, compact infrared
 Endress+Hauser
Flowfit CUA252
 Endress+Hauser